Bel-Ray® Is The Clear Choice For Food And Beverage Operators

PC-12 Is Coming: What The Next Generation Of Heavy-Duty Diesel Engine Oil Means For Your Fleet
November 5, 2026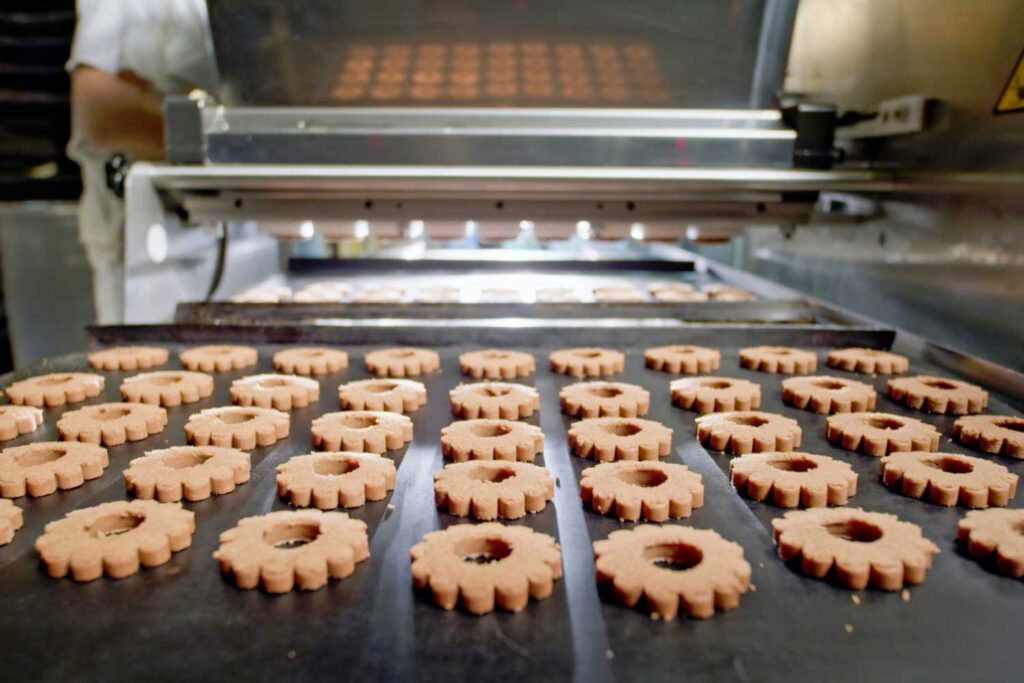
In food and beverage processing, lubricants have two critical jobs: protect equipment and protect product integrity. That can be a demanding combination in facilities where frequent washdowns, high humidity, and the possibility of incidental food contact are part of everyday operations.
Bel-Ray® No-Tox® Food Grade Clear Grease is engineered specifically for these challenging environments. It delivers dependable equipment protection while meeting the stringent requirements of food and beverage operations.
Stays Put When The Water Starts Flowing
Water is unavoidable in food and beverage plants. Frequent sanitation cycles, wet processing areas, and humid conditions can quickly wash away lubricants that aren’t designed for the environment. When that happens, components can be left vulnerable to wear, rust, and corrosion.
No-Tox Food Grade Clear Grease is formulated to resist water washout and maintain a protective lubricating film on plain and antifriction bearings, slides, guides, and other moving components even in areas exposed to significant moisture.
Its performance is driven by the factors below.
- Excellent water resistance: An aluminum complex thickener helps the grease resist washout and stay where it’s needed during wet operating conditions and washdowns.
- Protection against rust and corrosion: Specially selected inhibitors help protect critical components in consistently wet and humid environments.
- Proven washout performance: In water-washout testing, the NLGI Grade 2 formulation recorded just 2.5% loss at 79° C (175° F). This helped demonstrate its ability to remain in place when exposed to water.
Clear By Design
Performance isn’t the only consideration on a food production line. Cleanliness and appearance matter, too.
No-Tox Food Grade Clear Grease features a clear appearance and smooth texture. That makes it particularly well-suited for applications where visible lubricant contamination is a concern. In the event of incidental contact with food products or packaging, its clear appearance helps minimize the staining and discoloration commonly associated with conventional dark or opaque greases.
The result is high-performance lubrication that helps protect equipment without compromising the clean appearance operators expect on the production line.
Food-Grade Protection You Can Count On
No-Tox Food Grade Clear Grease combines water resistance and equipment protection with the certifications and performance characteristics demanded by today’s food and beverage facilities.
- Microbial resistance: Bacteriological protection helps inhibit the growth of certain bacteria, yeast, and mold within the grease.
- Wide operating temperature range: Provides reliable performance from -20° C to 177° C (-4° F to 350° F) across a broad range of processing applications.
- Food-grade compliance: Meets FDA requirements under Title 21 CFR 178.3570, and is NSF H1 registered for applications where incidental food contact may occur.
- Third-party certifications: ISO 21469 certified and Kosher, Pareve, and Halal-approved. Helps support demanding food-safety and quality programs.
Protection That Performs In Demanding Food-Processing Environments
In wet and washdown-intensive areas, the right lubricant can help reduce washout, protect against corrosion, maintain reliable equipment performance, and support stringent food-safety requirements. Bel-Ray® No-Tox® Food Grade Clear Grease delivers the combination of water resistance, equipment protection, cleanliness, and food-grade assurance that operators need to keep production moving.
Contact the Bel-Ray team to learn more about No-Tox Food Grade Clear Grease or to discuss a lubrication program tailored to the needs of your food and beverage operation.
